Discover high-density engineered composites, book-matched natural stone slabs, and structural exterior veneers tested to the most demanding international architectural standards.
Two Decades of Engineering Excellence, Global Logistics Precision, and Resource Stewardship.
Foshan Aura Stone Co., Ltd. was established in Foshan, China, in 2005. Over the past 20 years, we have grown into a leading supplier and exporter of high-quality building materials and stone products, serving customers in more than 150 countries worldwide.
With two decades of experience, we have accumulated rich industry knowledge and extensive global customer resources. In recent years, the company has focused on upgrading its core competitiveness, investing in mining resource development, intelligent production technologies, and the processing of finished products. Transitioning from a trade-oriented company to a comprehensive import and export enterprise, we now offer integrated solutions that meet the highest international standards.
Our products have been applied in numerous significant projects worldwide, including prestigious government and commercial developments, such as large-scale urban renovation projects in Switzerland, national cemetery constructions in Russia, subway stations in the Netherlands, and many high-end hotel and villa projects through long-term partnerships with distributors and construction supply chains.
Demystifying Cryptocrystalline Mineralogy, High-Yield Structural Honeycomb Backing, and Photometric Backlighting Architecture.
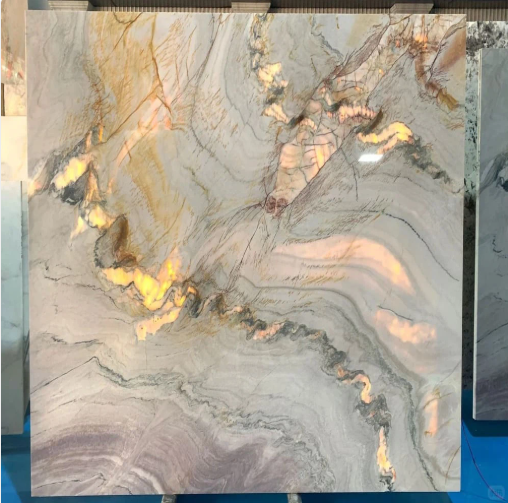
True natural onyx is a parallel-banded variety of silicate chalcedony, while architectural commercial onyx predominantly consists of translucent cryptocrystalline banded calcite or aragonite. Our extraction engineering targets geological formations exhibiting calcite purity surpassing 98.4%, ensuring supreme light transmittance coefficients (tau) ranging between 0.32 and 0.68 without organic macro-porosity.
Due to the inherently fragile crystalline structure of natural onyx, monolith slabs thicker than 20mm represent unsustainable structural dead-weight. Foshan Aura Stone implements patented 5mm ultra-thin slicing coupled with aerospace aluminum honeycomb (AA3003/AA5052) or optical tempered glass backing using aerospace-grade epoxy resins, increasing flexural modulus (Ru) by over 450%.
Translucency demands systemic photometric alignment. Our engineering advisory defines precise diffusion distances (minimum 60mm–120mm air-gap) and integrates LED light sheet arrays calibrated from 2700K (warm amber dispersion) to 6500K (crisp crystalline arctic luminescence). CRI values >95 are strictly specified to eliminate chromatic aberration across contiguous book-matched seams.
Navigating Raw Quarry Concessions, Geopolitical Logistics Risk, and Universal Building Codes.
Every commercial consignment exported from Foshan Aura Stone adheres to ASTM C503 (Standard Specification for Marble Dimension Stone), ASTM C880 (Flexural Strength), and EN 1469 (Natural Stone Products for Cladding). Hydrostatic water absorption coefficients are rigorously contained below 0.15%, preventing moisture-induced shadow lines when interacting with architectural adhesives.
In accordance with global green building mandates (USGBC LEED v4.1, BREEAM, and DGNB), our low-impact diamond-wire quarrying methods and closed-loop hydraulic recycling reduce carbon embodied intensity per m² by 38% compared to industry averages. Full Environmental Product Declarations (EPDs) and zero-VOC lamination resins facilitate seamless qualification for platinum-tier green architecture.
Maritime export of high-fragility translucent onyx necessitates specialized multi-layer crating protocols. We construct fumigated ISPM-15 compliant hardwood A-frames equipped with continuous neoprene buffering, moisture-desiccant matrices, and single-use digital tri-axial shock/tilt sensors (TiltWatch/ShockWatch) to ensure pristine transit across high-seas corridors.
Transforming Prestigious Public Works, Ultra-Luxury Commercial Portals, and Private Havens into Timeless Masterpieces.
From the iconic 5-star grand lobbies of Dubai, Zurich, and Singapore to intimate executive lounges, our backlit translucent onyx columns and reception counters establish sensory focal points. By marrying custom CNC-milled 45-degree mitered edges with rear-accessible LED maintenance trays, we guarantee operational longevity in 24/7 public environments.
Marine naval architecture demands radical weight containment without conceding opulent visual prestige. Our ultra-thin 3mm honeycombed onyx composites fulfill IMO (International Maritime Organization) FTP Code flammability and smoke criteria, lowering bulkhead bulk load by up to 70% compared to traditional 20mm dimensional slabs on mega-yacht staterooms.
Translucency evokes spiritual resonance and institutional gravitas. Building on our demonstrated execution in European subway networks and state cemetery projects in Russia, our precision cut-to-size onyx panels function as acoustic-dampened sacred walls, altars, and backlit monolithic memorial plinths designed to endure environmental cycling.
Pioneering Computer Vision Dry-Lay Systems, Micro-Polymer Vacuum Impregnation, and Smart IoT Stone Surfaces.
Manual slab layout introduces subjective errors on complex multi-thousand-square-meter projects. Our automated optical scanners map chromatic banding, veining trajectory, and micro-fractures into 4K digital twins. AI neural algorithms then calculate the optimal book-matching, diamond-matching, or butterfly configurations, generating real-time BIM files prior to the initial waterjet cut.
Micro-crystalline fissure stabilization is paramount for natural onyx integrity. Our production lines deploy hyper-baric vacuum tanks operating at -0.1 MPa to evacuate entrapped gases from slab micro-pores, backfilling with UV-stabilized, non-yellowing fluorocarbon polyurethane resins that match the precise refractive index of natural calcite (1.486 to 1.658).
Looking to 2026 and beyond, Foshan Aura Stone is engineering embedded low-heat thin-film conductive traces within composite onyx substrates. This facilitates direct touch-capacitive controls, variable chromatic circadian rhythms synchronized with local astronomical sunrise/sunset cycles, and structural thermal insulation improvements exceeding traditional stone envelopes.
Synthesizing Sustainable Architecture, Technological Innovation, and Uncompromising Craftsmanship.
In the past five years, with rising quality and service expectations in the domestic market, Foshan Aura Stone has expanded its cooperation with premium hotels and major engineering companies, providing export-quality products and services domestically. This strategy has allowed us to combine global experience with local excellence, ensuring that each project is executed to the highest standards.
We adhere to the corporate values of responsibility, progress, gratitude, and happiness, with a mission to cultivate professional expertise within our team. Our vision is to make architecture worldwide more beautiful and sustainable. Through dedicated service and collaborative innovation, we have earned the trust and recognition of customers across the globe, establishing long-term, win-win partnerships.
Foshan Aura Stone Co., Ltd. continues to advance in technology, design, and global partnerships, committed to creating a lasting impact on the construction and stone industry worldwide.
Authoritative Answers to Mission-Critical Technical Inquiries for Project Managers, Specifiers, and Stone Contractors.
In high-end architectural dimension stone terminology, "onyx" denotes translucent, cryptocrystalline banded calcite or travertine varieties rather than true black silica onyx (a chalcedony variant). Calcite onyx possesses alternating crystalline layers that create unique natural depth and light refraction properties when backlit, with Mohs hardness typically ranging from 3.0 to 4.0.
Enclosed LED backlighting creates localized heat build-up. Monolithic 20mm onyx exposed to continuous radiant thermal differential can experience bowing or fissure expansion. By laminating 5mm onyx to 15mm tempered ultra-clear glass or structural honeycomb with matched coefficients of thermal expansion (CTE), stress is distributed evenly, eliminating thermal fatigue and panel distortion.
For heavy footfall lobbies and commercial plazas, unreinforced natural onyx is rarely recommended for raw flooring. However, our laminated glass-onyx or sintered stone composites achieve flexural breaking loads exceeding 4,500 N and compressive strengths over 110 MPa, easily surpassing EN 1341 and ASTM C880 standards for luxury commercial floor traffic.
We mandate high-resolution 5-axis CNC bridge-sawing and robotic waterjet machining to preserve continuous vein trajectories across panel splits. Dimensional cutting tolerance is maintained within ±0.5mm, and slab thickness tolerance within ±0.3mm. Every slab sequence is photogrammetrically pre-matched in CAD/BIM space and pre-assembled in our facility for client sign-off.
Because calcite onyx is sensitive to acidic etching and solvent discoloration, we exclusively recommend deep-penetrating fluoro-chemical impregnators that remain chemically inert under LED ultraviolet emissions. These nano-molecular sealers preserve open vapor transmission while achieving high oleophobic and hydrophobic surface repellency.
All Foshan Aura Stone export containers include verified Mill Test Certificates, ASTM/CE Testing Dossiers, fumigation phytosanitary certification (ISPM-15), country of origin declarations, digital dry-lay mapping sheets, and installation schematics indexing each crated piece to the architect's approved elevations.
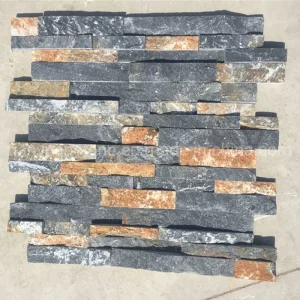
From flame-resistant basalt composite fibers to precision nano-crystallized glass surfaces and hand-dressed ledger stone panels.
 Aura Stone