Explore our precision-crafted natural stones, advanced artificial surfaces, and specialized industrial mineral powders designed for global engineering projects.
Foshan Aura Stone Co., Ltd. was established in Foshan, China, in 2005. Over the past 20 years, we have grown into a leading supplier and exporter of high-quality building materials and stone products, serving customers in more than 150 countries worldwide.
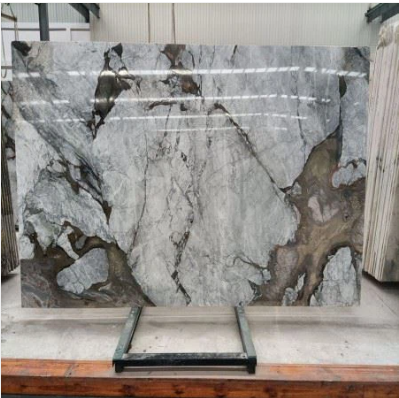
With two decades of experience, we have accumulated rich industry knowledge and extensive global customer resources. In recent years, the company has focused on upgrading its core competitiveness, investing in mining resource development, intelligent production technologies, and the processing of finished products. Transitioning from a trade-oriented company to a comprehensive import and export enterprise, we now offer integrated solutions that meet the highest international standards.
Our products have been applied in numerous significant projects worldwide, including prestigious government and commercial developments, such as large-scale urban renovation projects in Switzerland, national cemetery constructions in Russia, subway stations in the Netherlands, and many high-end hotel and villa projects through long-term partnerships with distributors and construction supply chains.
In the past five years, with rising quality and service expectations in the domestic market, Foshan Aura Stone has expanded its cooperation with premium hotels and major engineering companies, providing export-quality products and services domestically. This strategy has allowed us to combine global experience with local excellence, ensuring that each project is executed to the highest standards.
We adhere to the corporate values of responsibility, progress, gratitude, and happiness, with a mission to cultivate professional expertise within our team. Our vision is to make architecture worldwide more beautiful and sustainable. Through dedicated service and collaborative innovation, we have earned the trust and recognition of customers across the globe, establishing long-term, win-win partnerships.
Foshan Aura Stone Co., Ltd. continues to advance in technology, design, and global partnerships, committed to creating a lasting impact on the construction and stone industry worldwide.
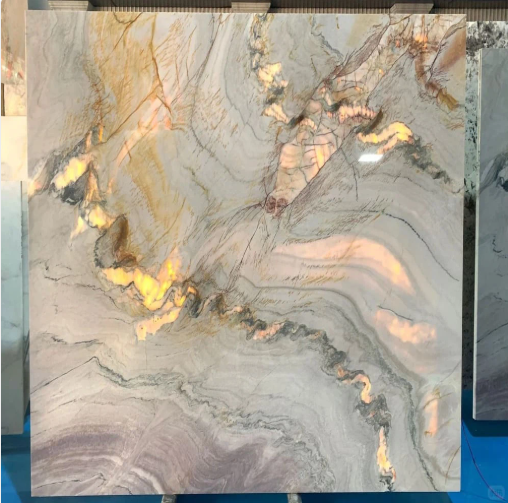
The global natural stone industry, specifically the segment dedicated to granite tile manufacturing, has experienced a tectonic shift towards high-precision automation, eco-conscious quarrying, and stringent supply chain traceability. As modern architecture demands materials that offer uncompromising structural integrity alongside aesthetic versatility, top-tier manufacturers are redefining traditional stone processing.
Granite remains the cornerstone of heavy-traffic commercial flooring, ventilated exterior facades, and municipal infrastructure due to its exceptional compressive strength, freeze-thaw resistance, and acid-alkali tolerance. Our research indicates that North American and European markets prioritize dimensional precision (calibrated thickness within ±0.5mm) and certified slip resistance (R11/R12 ratings), driving factories in key production hubs to adopt multi-wire diamond saws and robotic flame-texturing lines.
Operating out of manufacturing powerhouses like Foshan grants industry leaders unique logistical and technological synergies. The Chinese stone processing ecosystem has transitioned from labor-intensive cutting to fully automated, IoT-integrated smart factories. This technological leap ensures unmatched volume scalability, rapid turnaround times, and strict batch consistency.
Supply chain resilience is anchored in integrated resource management—from direct block selection at international quarries (in India, Brazil, Norway, and South Africa) to high-speed polishing lines and eco-friendly water recycling systems. By maintaining strategic buffer inventories of raw blocks and finished tiles, top manufacturers insulate international contractors from raw material volatility and global shipping disruptions.
Granite tiles exhibit extraordinary adaptability across diverse geographical and architectural typologies:
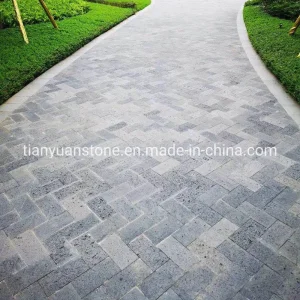
1. Heavy-Traffic Urban Infrastructure: In municipal pedestrian zones, subway platforms (such as our referenced Dutch infrastructure projects), and airport concourses, flamed or bush-hammered granite tiles prevent slippage under wet conditions while withstanding millions of footfalls annually.
2. High-End Commercial Facades: Ventilated curtain wall systems utilizing lightweight, thin granite panels provide superior thermal insulation and wind-load resistance for skyscrapers across European urban centers.
3. Luxury Residential & Hospitality: Polished black, grey, and white granite tiles serve as timeless interior flooring and kitchen countertops, offering thermal shock resistance and effortless maintenance in luxury villas and five-star hotels.
The next decade of granite tile manufacturing will be defined by sustainability and nano-technological surface enhancement. Key pillars of our R&D roadmap include:
Zero-Waste Quarrying & Processing: Implementing closed-loop water filtration systems that recycle 98% of industrial wastewater, alongside converting stone slurry into eco-friendly building bricks.
Nano-Coated Self-Cleaning Surfaces: Integrating photocatalytic titanium dioxide nanoparticles into exterior granite tiles to break down organic pollutants and neutralize urban smog.
AI-Powered Optical Quality Control: Deploying machine learning algorithms and high-resolution optical scanners to detect micro-fissures and color tone variations instantly during high-speed production.
Navigating international building codes requires rigorous third-party testing and documentation. Foshan Aura Stone maintains active compliance with international standards, including CE marking for European structural applications, ASTM C615 specifications for North American granite, and ISO 9001 quality management certifications.
Our multilingual engineering support team collaborates directly with local architects, structural consultants, and importing distributors from the initial design phase to final site delivery. We provide comprehensive technical dossiers, including slip-resistance certificates, petrographic analysis reports, and customized dry-lay mapping services to guarantee seamless installation.
Discover more specialized surfacing solutions tailored for interior detailing, wall cladding, and high-end exterior landscaping.
Expert insights into granite tile sourcing, manufacturing standards, and global project execution.
 Aura Stone