Explore our primary selection of premium quartzite slabs, customized terrazzo, and sintered stone tiles engineered for extreme durability and aesthetic perfection.
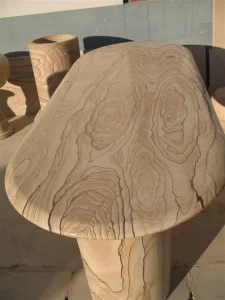
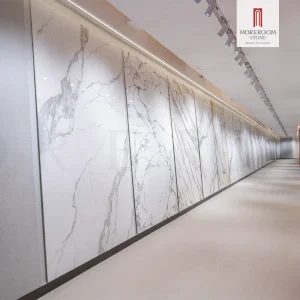
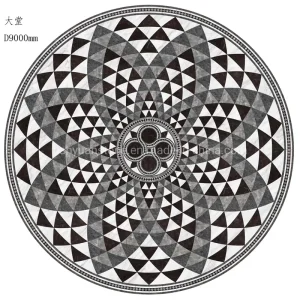
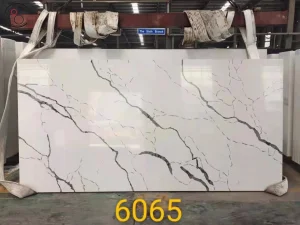
The global stone market has undergone a paradigm shift over the past decade. Natural quartzite—a metamorphic rock formed originally from pure quartz sandstone through high-temperature and high-pressure tectonic forces—has emerged as the premier choice for tier-one global infrastructure, luxury commercial complexes, and ultra-high-end residential projects. Unlike standard granites or softer marbles, natural quartzite boasts a Mohs hardness rating of 7, exceptional silica density, and extreme chemical inertness, making it virtually impervious to acidic etching, thermal shock, and heavy mechanical abrasion.
Simultaneously, advancements in material science have propelled engineered quartz and sintered stone matrices into the architectural spotlight. China has positioned itself as the international epicenter for advanced stone processing, quarrying investments, and supply chain digitization. As the world’s leading hub for quartz manufacturing, China’s industrial ecosystem combines automated multi-wire diamond sawing, vacuum resin resinification, ultra-thin calibration technology, and 5-axis CNC waterjet carving.
Commercial contractors and architectural procurement heads no longer look at stone merely as a decorative surfacing layer. Today, structural integrity, long-term non-porous performance, low life-cycle maintenance costs, and carbon-footprint credentials govern specification decisions. Chinese quartzite suppliers lead this transformation by pairing localized mineral wealth with global logistics integration, supplying millions of square meters of dimension stone annually to Europe, North America, the Middle East, and Southeast Asia.
Foshan Aura Stone Co., Ltd. was established in Foshan, China, in 2005. Over the past 20 years, we have grown into a leading supplier and exporter of high-quality building materials and stone products, serving customers in more than 150 countries worldwide.
With two decades of experience, we have accumulated rich industry knowledge and extensive global customer resources. In recent years, the company has focused on upgrading its core competitiveness, investing in mining resource development, intelligent production technologies, and the processing of finished products. Transitioning from a trade-oriented company to a comprehensive import and export enterprise, we now offer integrated solutions that meet the highest international standards.
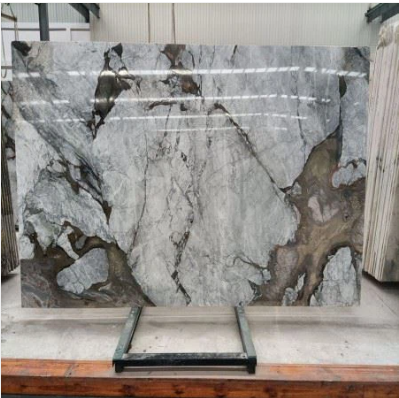
Our products have been applied in numerous significant projects worldwide, including prestigious government and commercial developments, such as large-scale urban renovation projects in Switzerland, national cemetery constructions in Russia, subway stations in the Netherlands, and many high-end hotel and villa projects through long-term partnerships with distributors and construction supply chains.
In the past five years, with rising quality and service expectations in the domestic market, Foshan Aura Stone has expanded its cooperation with premium hotels and major engineering companies, providing export-quality products and services domestically. This strategy has allowed us to combine global experience with local excellence, ensuring that each project is executed to the highest standards.
We adhere to the corporate values of responsibility, progress, gratitude, and happiness, with a mission to cultivate professional expertise within our team. Our vision is to make architecture worldwide more beautiful and sustainable. Through dedicated service and collaborative innovation, we have earned the trust and recognition of customers across the globe, establishing long-term, win-win partnerships.
Foshan Aura Stone Co., Ltd. continues to advance in technology, design, and global partnerships, committed to creating a lasting impact on the construction and stone industry worldwide.
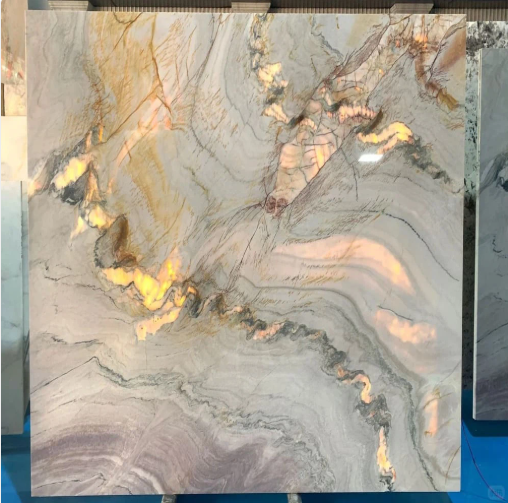
The global stone fabrication sector is navigating a major technological revolution. Buyers, specifiers, and master builders require higher technical compliance, zero-defect slabs, and strict traceabilities. Below are the key structural shifts shaping China's quartzite export market:
Modern fabrication uses high-definition 3D laser imaging and AI algorithms to scan natural vein structures. This allows computer-aided dry-lay mockups prior to cutting, enabling flawless continuous vein mapping across massive commercial facades and interior features.
Bridging the gap between pure geology and industrial manufacturing, high-pressure sintering (over 15,000 tons of compaction force) combines pure quartzite minerals with micro-crystalline glass matrixes for zero-porosity, non-staining cladding elements.
Environmental management is now integral to exporting stone globally. Leading Chinese exporters utilize closed-loop water filtration systems that recycle 98% of stone-cutting slurry, coupled with solar-powered processing plants.
To ensure optimal engineering performance across various climates and stress environments, Foshan Aura Stone subjects all quartzite, marble, and sintered materials to rigorous physical testing under international testing regimes (ASTM, EN, and ISO standards).
| Physical / Mechanical Property | Natural Quartzite Standard | Engineered Quartz Matrix | Sintered Stone Slab | Testing Standard (ISO / ASTM) |
|---|---|---|---|---|
| Mohs Hardness Grade | 7.0 - 7.5 | 6.5 - 7.0 | 7.0 - 8.0 | ASTM C1895 / EN 101 |
| Water Absorption Rate (%) | ≤ 0.15% | ≤ 0.03% | ≤ 0.01% | ASTM C97 / ISO 10545-3 |
| Compressive Strength (MPa) | 180 - 250 MPa | 200 - 240 MPa | ≥ 300 MPa | ASTM C170 / EN 1926 |
| Flexural Strength (Modulus of Rupture) | 20 - 35 MPa | 35 - 50 MPa | 45 - 65 MPa | ASTM C99 / ISO 10545-4 |
| Abrasion Resistance (mm³) | High (≤ 135 mm³) | Superior (≤ 110 mm³) | Ultra High (≤ 90 mm³) | EN 14157 / ASTM C1353 |
| Chemical & Stain Resistance | Unaffected by mild acids | Stain Proof (Resin Bonded) | Completely Chemical Inert | ASTM C650 / ISO 10545-13 |
Processing natural quartzite requires advanced tool mechanics due to its exceptionally high silica content and density. Standard gang saws used for marble fail when cutting quartzite blocks. Foshan Aura Stone implements a comprehensive fabrication methodology:
Utilizing high-concentration diamond beads wired under 45-50 kN tension, allowing precise block slabbing with zero internal micro-fracturing.
Slabs are introduced into 5-bar vacuum chambers where high-penetration bio-resins fill micro-fissures, reinforcing long-term structural stability.
Incorporating garnet abrasive waterjets operating at 4,000 bar pressure for exact complex curves, medallions, and interlocked custom joinery.
From heavy public infrastructure subject to foot traffic from millions of commuters to high-end residential interiors requiring aesthetic distinction, our product portfolio provides specific engineering benefits:
Applied in public infrastructure such as Netherlands subway stations, our ultra-dense paving tiles offer slip-resistant surface finishes (R11 ratings), superior flexural loading resilience, and easy maintenance against oil and dirt accumulation.
Engineered to withstand freeze-thaw cycles without spalling, our premium quartz and granite products were chosen for large-scale urban renovations in Switzerland and national cemetery developments in Russia, delivering multi-decadal weather resistance.
In luxury hotels, high-end background walls, and vanity counters, materials like translucent waterjet marble medallions, nano-crystallized glass, and exotic natural quartzite slabs deliver distinctive aesthetic appeal alongside chemical stain resistance.
Procuring building materials across international borders presents complex logistics, specification, and quality-assurance challenges. Foshan Aura Stone addresses these friction points with comprehensive B2B supply-chain engineering:
We manage original quarry concessions and direct mining allocations worldwide. By reserving entire quarry faces, we guarantee tone, grain, and color consistency across commercial projects scaling over 50,000 square meters.
All slabs and cut-to-size elements undergo ISPM 15 compliant fumigated wooden bundling, reinforced with A-frame steel racks, shock-absorption foam linings, and corner plastic protections for ocean transport safety.
Our manufacturing plants run on energy-efficient smart grids and low VOC resin formulations. Our products contribute toward LEED v4 credits for Material & Resources (MR) and Indoor Environmental Quality (EQ).
Expert insights on selecting, installing, and procuring natural quartzite and engineered stone from China's leading exporter.
Natural Quartzite is a metamorphic rock formed from quartz sandstone subjected to extreme heat and pressure; it features a Mohs hardness of 7 and natural veining. Granite is an igneous rock with a granular structure composed of quartz and feldspar (Mohs 6-7). Artificial or Engineered Quartz consists of roughly 90-93% crushed quartz bound with resin pigments. Sintered stone is 100% natural mineral pressed and fired at high temperatures (>1200°C) with no resin content.
Foshan is recognized globally as the center of advanced stone processing and ceramic/sintered technology. Sourcing from Foshan Aura Stone provides access to advanced 5-axis CNC processing, competitive batch pricing, strict quality assurance, and end-to-end export management refined across 20 years of global project delivery in over 150 countries.
While natural quartzite is highly resistant to acid etching and scratch damage, high-grade penetrating sealers should be applied during installation. This protects against micro-porous absorption along seam lines and preserves optimal stain resistance over long operational lifespans in commercial kitchens and high-traffic areas.
We implement automated digital scanning and AI vein-matching software. By pre-laying slabs virtually in CAD models prior to waterjet precision cutting, we maintain continuous pattern alignment, strict batch tint tolerance, and dry-lay approval protocols for project owners prior to final crate packing.
Standard slab sizes include 3200x1600mm, 3000x1000mm, and 1200x2600mm, with thicknesses ranging from 3mm and 6mm (for light wall cladding) to 12mm and 20mm (for structural floor loads and heavy countertops). Available finishes include Polished, Honed, Leathered/Antique, Flamed, and Bush-hammered.
Discover our extended series of Roman travertine, custom Calacatta sintered slabs, natural marble mosaics, basalt tiles, and architectural wall veneers.
 Aura Stone